Rebaudioside M Powder
Description
Rebaudioside M Powder: Premium Biosynthesized Stevia Sweetener for Next-Generation Food & Beverage Formulations
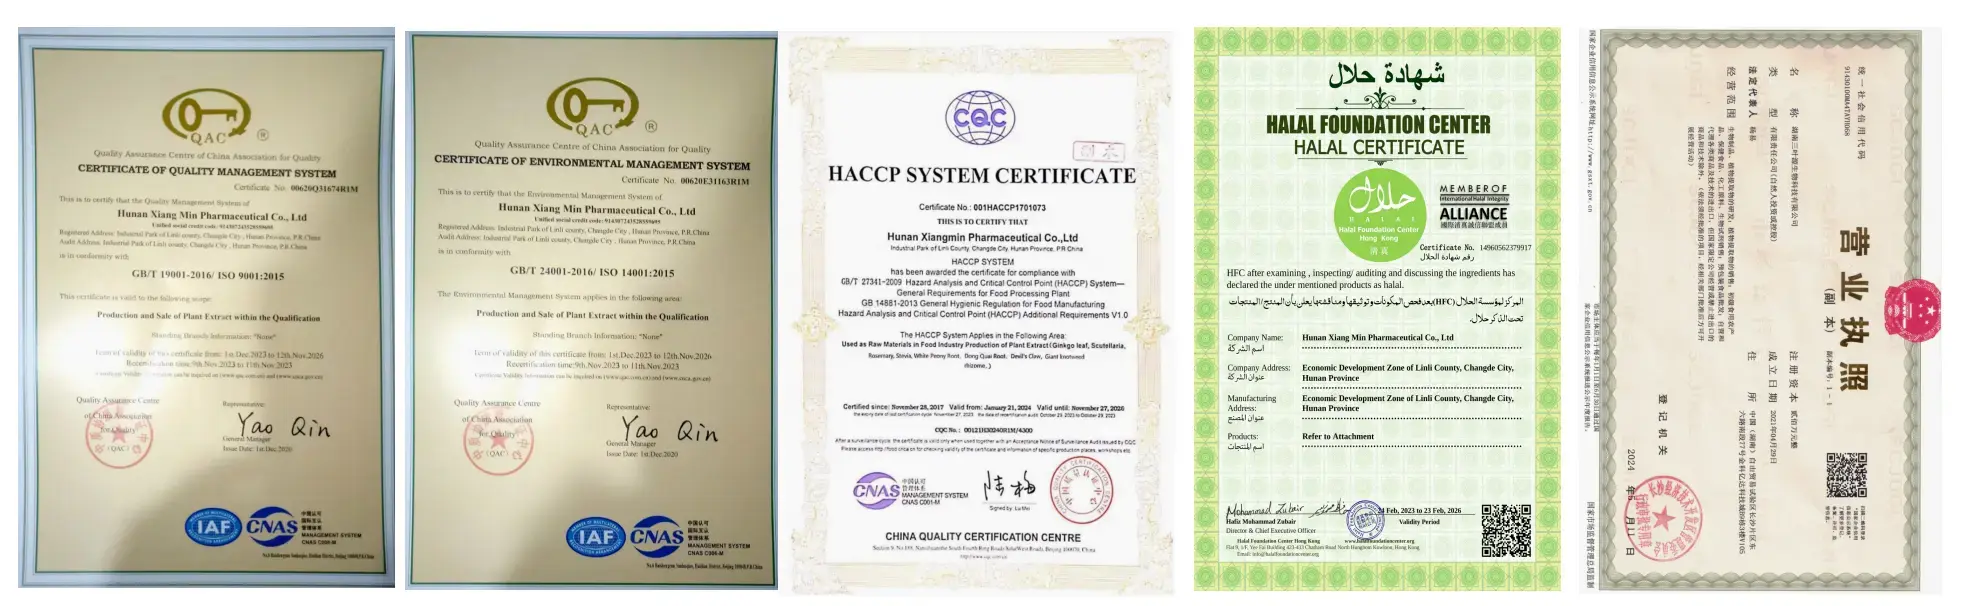
Hunan Clover Origins Biotech's Rebaudioside M Powder features the highest purity in the industry with ≥96% Reb M content, achieved by superior biosynthesis technology. Our production capacity exceeds 5,000 tons per year and we are certified by FDA, ISO 9001, HACCP and FSSC 22000. We offer consistent supply chain economics and improved flavor profiles that outperform standard Reb A. Our fermentation-based production process ensures consistent quality batch to batch, with low levels of bitterness and licorice aftertaste, making it excellent for beverage reformulation and sugar-reduction methods. With 25+ years of botanical extract knowledge, we provide flexible MOQ, fast sampling in 7 days, and technical support during your product development cycle.
What Makes Our Rebaudioside M Powder Stand Out?
Rebaudioside M (also known as Reb M or Rebaudioside A3) is the next evolution in stevia sweetening technology. Our biosynthetic process, designed for yeast fermentation, is unparalleled in purity and flavor consistency compared to standard leaf extraction methods.
The main difference is the way they are made. At scale, making it by fermentation is cheaper than extracting it from the plant. You receive consistent ≥96% Reb M purity in every batch, so you don't have to worry about compositional variability that plagues leaf-derived products.
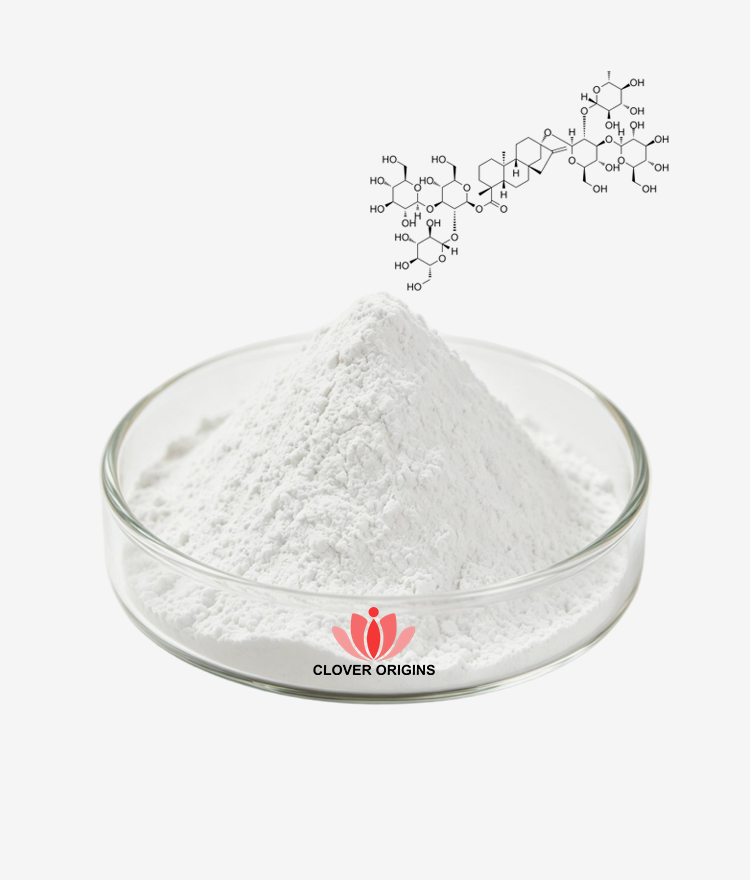
Our white to off-white powder (CAS No. 1220616-44-3) is readily soluble in formulas. It gives you 200-300x the sweetness of sucrose depending on your application matrix. This means you can reach the appropriate sweetness level with the minimum amount of dosage.
Technical Specifications & Quality Parameters
| Parameter | Specification |
|---|---|
| Product Name | Rebaudioside M Powder |
| Alternative Names | Reb M, Rebaudioside A3, Steviol Glycoside Reb M |
| Purity | ≥96% Rebaudioside M |
| Test Method | HPLC |
| CAS Number | 1220616-44-3 |
| Appearance | White to off-white powder |
| Production Process | Biosynthesis (Fermentation) |
| Sweetness Intensity | 200–300× sucrose |
| Caloric Content | Zero calories |
| Heat Stability | Stable under pasteurization/UHT |
| pH Stability | Stable in acidic conditions (pH 2.5–4.0) |
| Origin | China |
| Certifications | FDA, ISO 9001, HACCP, FSSC 22000, Kosher, Halal |
Superior Taste Profile: The Real Game-Changer
Why are large beverage businesses moving to Rebaudioside M Powder? The answer is simple: flavor.
Consumers dislike the bitter, metallic aftertaste of traditional stevia extracts, such as Reb A. Reb M is the answer to the dilemma. Its sweetness profile is similar to sucrose and it has almost no bitterness or licorice off flavors.
Clean finish, suited for large dosage sweetening systems. No masking chemicals or flavor modulators are required. This reduces your ingredient deck and allows for clean label positioning.
For product developers , this means speedier formulation cycles. Your sensory panels will approve formulas faster. Reach the market faster, while preserving the sugar-free positioning your clients are looking for.
Broad Application Spectrum Across Multiple Categories
Beverages are the greatest application category for Rebaudioside M. Our powder's great solubility and stability are benefits for carbonated soft drinks, functional wellness drinks, RTD tea and coffee, and juice blends.
Many formulators blend Reb M with Reb D or erythritol to achieve the best taste balance. Our technical staff can help you with ratio optimization to meet your individual product requirements.
Health and nutrition items are another significant growth area. The zero-calorie, zero-glycemic effect features are beneficial for weight control supplements, protein powders, meal replacement drinks and effervescent tablets. Metabolic neutrality is very useful for diabetic-friendly formulations.
Our powder is being used more in reduced sugar yogurts, flavored almond milk, oat beverages and soy drinks, in dairy and plant-based alternatives. The heat stability ensures that the sweetness remains without deterioration during pasteurization operations.
Bakery, confectionery and pharmaceutical uses keep growing. The non-cariogenic sweetening qualities are used in sugar-reduced bakery products, chewing gum, diabetic syrups and chewable tablets. Our powder keeps its sweet profile through baking procedures.
Manufacturing Excellence & Quality Assurance
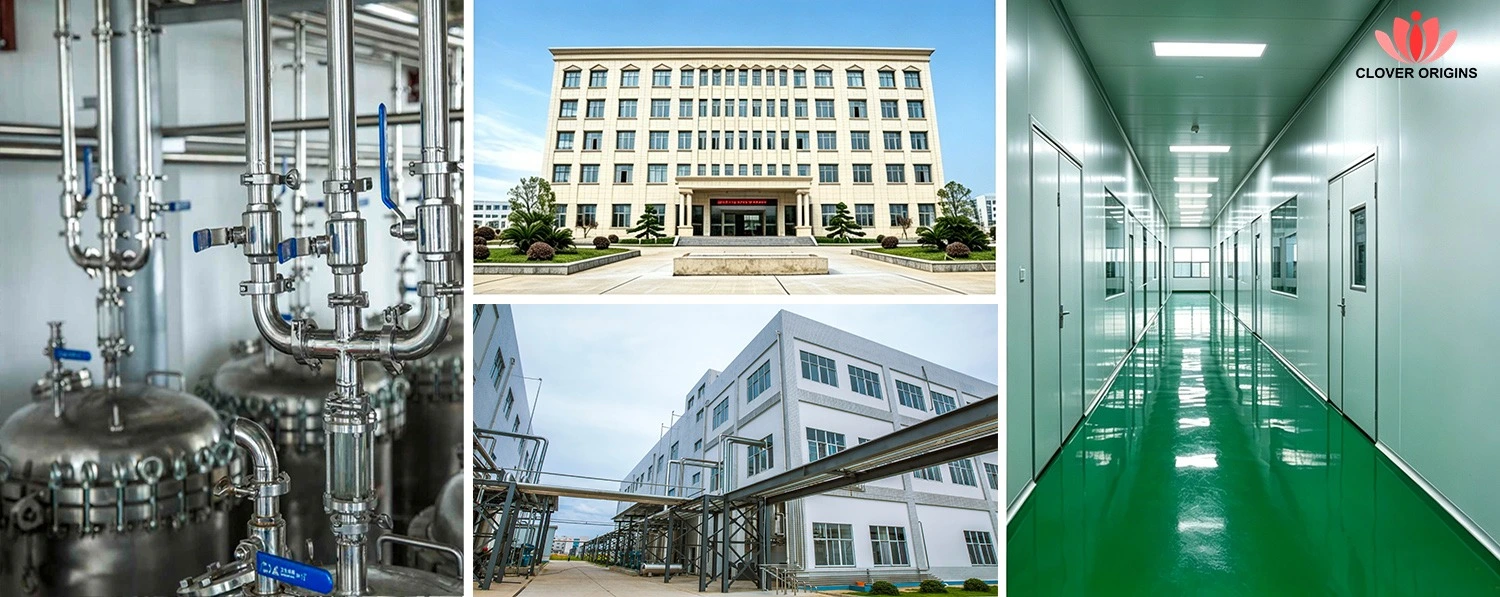
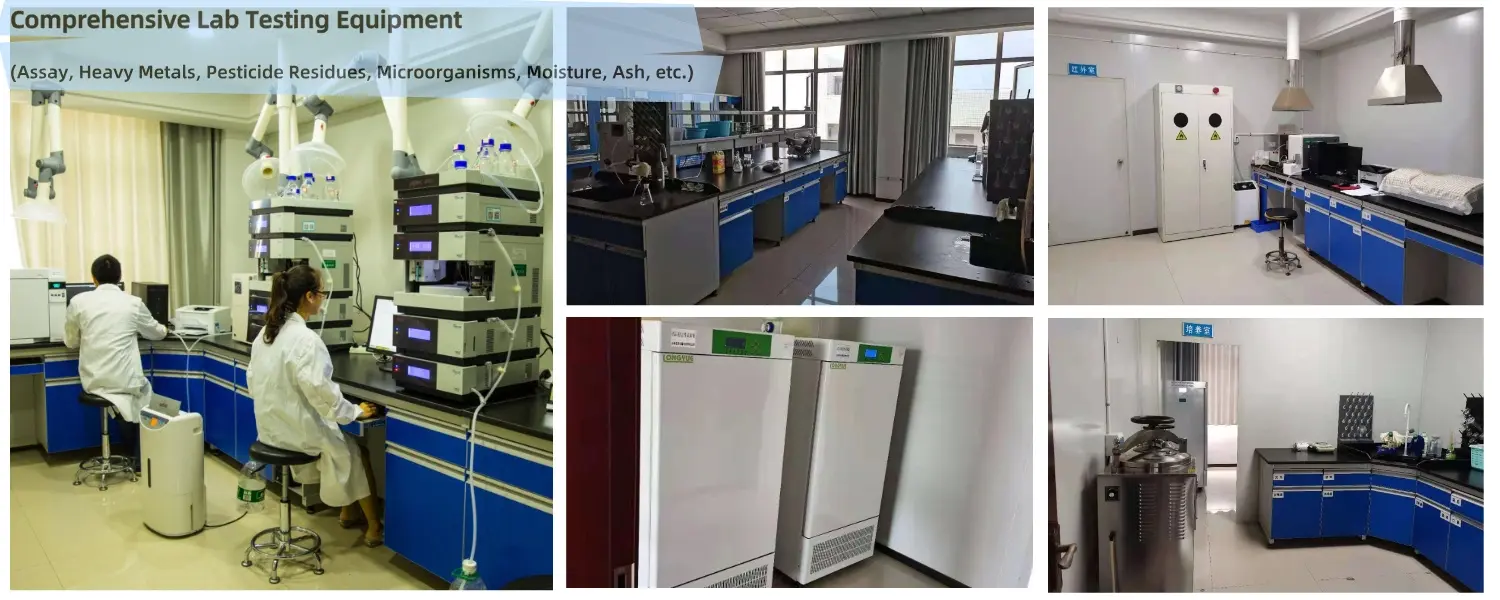
We have three modern production facilities operating under rigorous quality management systems. Every batch undergoes rigorous testing by in-house laboratories and third-party verification partners such as Eurofins, SGS and Alkemist Labs.
Regulatory compliance through complete traceability from source ingredients to finished goods. We test for active ingredients, heavy metals, microbiological pollutants, pesticide residues and ethylene oxide. Results meet or exceed standards in China, the European Union and the United States.
Standard goods ship from stock in 1-2 days. Custom specs are available with a 5-10 day manufacture lead time. Flexible MOQ to enable pilot testing and commercial-scale orders.
Technical documentation provided within 12 hours of request. We assist your product registration needs globally with Certificates of Analysis, specification sheets, allergen statements and regulatory compliance paperwork.
Supply Chain Reliability & Customer Partnership
Stable supply even during market changes with an annual production capacity over 5,000 tons. Responsive production scheduling and long-term inventory planning keep your formulation timetables on track.
We have a global logistics network including DHL, FedEx, UPS and TNT to deliver samples quickly. Commercial shipments can benefit from competent freight forwarders who can efficiently navigate customs clearance across numerous regulatory countries.
We'll react to your requests within 1 hour during business hours. We have a skilled technical support team ready to assist you throughout your product development cycle, from initial concept to scale up manufacture. Sample development is completed within 7 working days.
This partnership model is more than a transactional relationship. We help you understand your market position, regulatory needs and formulation issues. Your success fuels our innovation roadmap.
FAQ
Q: How does Reb M differ from Reb A in taste?
A: Reb M has significantly lower bitterness and no licorice aftertaste compared to Reb A. It provides a cleaner, more sucrose-like sweetness profile, which is why premium beverage brands are transitioning to Reb M formulations.
Q: Is biosynthesized Reb M considered natural for labeling purposes?
A: Regulatory treatment varies by region. In the US, fermentation-derived Reb M may be labeled as "stevia" or "steviol glycosides" under current FDA guidance. We provide region-specific labeling recommendations and compliance documentation.
Q: What is the typical usage level in beverages?
A: Dosage varies by desired sweetness and application, typically ranging from 50–200 mg/L for beverages. Our technical team can recommend precise levels based on your sugar equivalent target and flavor profile.
Q: Does the powder require special storage conditions?
A: Store in a cool, dry place away from direct light. The powder is stable under normal warehousing conditions. We recommend keeping containers sealed to prevent moisture absorption.
Q: Can you provide samples for formulation trials?
A: Yes, we offer free samples with professional technical consultation. Sample requests are processed within 7 working days, including international shipping.
Q: What documentation do you provide for regulatory compliance?
A: We supply Certificates of Analysis, specification sheets, allergen statements, BSE/TSE declarations, GMO status, and region-specific compliance documents. Third-party testing reports from Eurofins, SGS, or other recognized labs are available upon request.
Q: Do you offer custom blends with other sweeteners?
A: Absolutely. Our R&D team specializes in custom compound formulations. We can develop Reb M blends with erythritol, Reb D, or other sweetening systems optimized for your specific application requirements.
Partner With a Trusted Industry Leader
Ready to reformulate with Rebaudioside M Powder? Contact our technical team at info@cloverorigins.com to request samples and discuss your formulation needs today.
Online Message
YOU MAY LIKE
High quality furniture manufacturer