Factory Capabilities
Experienced R&D and Quality Assurance Team
With over 25 years of experience in botanical extract R&D, production, and global sales, our professional team provides technical support from raw material selection and formulation development to process optimization and quality testing.
We work closely with academic institutions and production bases to continuously improve product quality, develop customized solutions, and respond quickly to customer requirements.


Modern Manufacturing Facilities
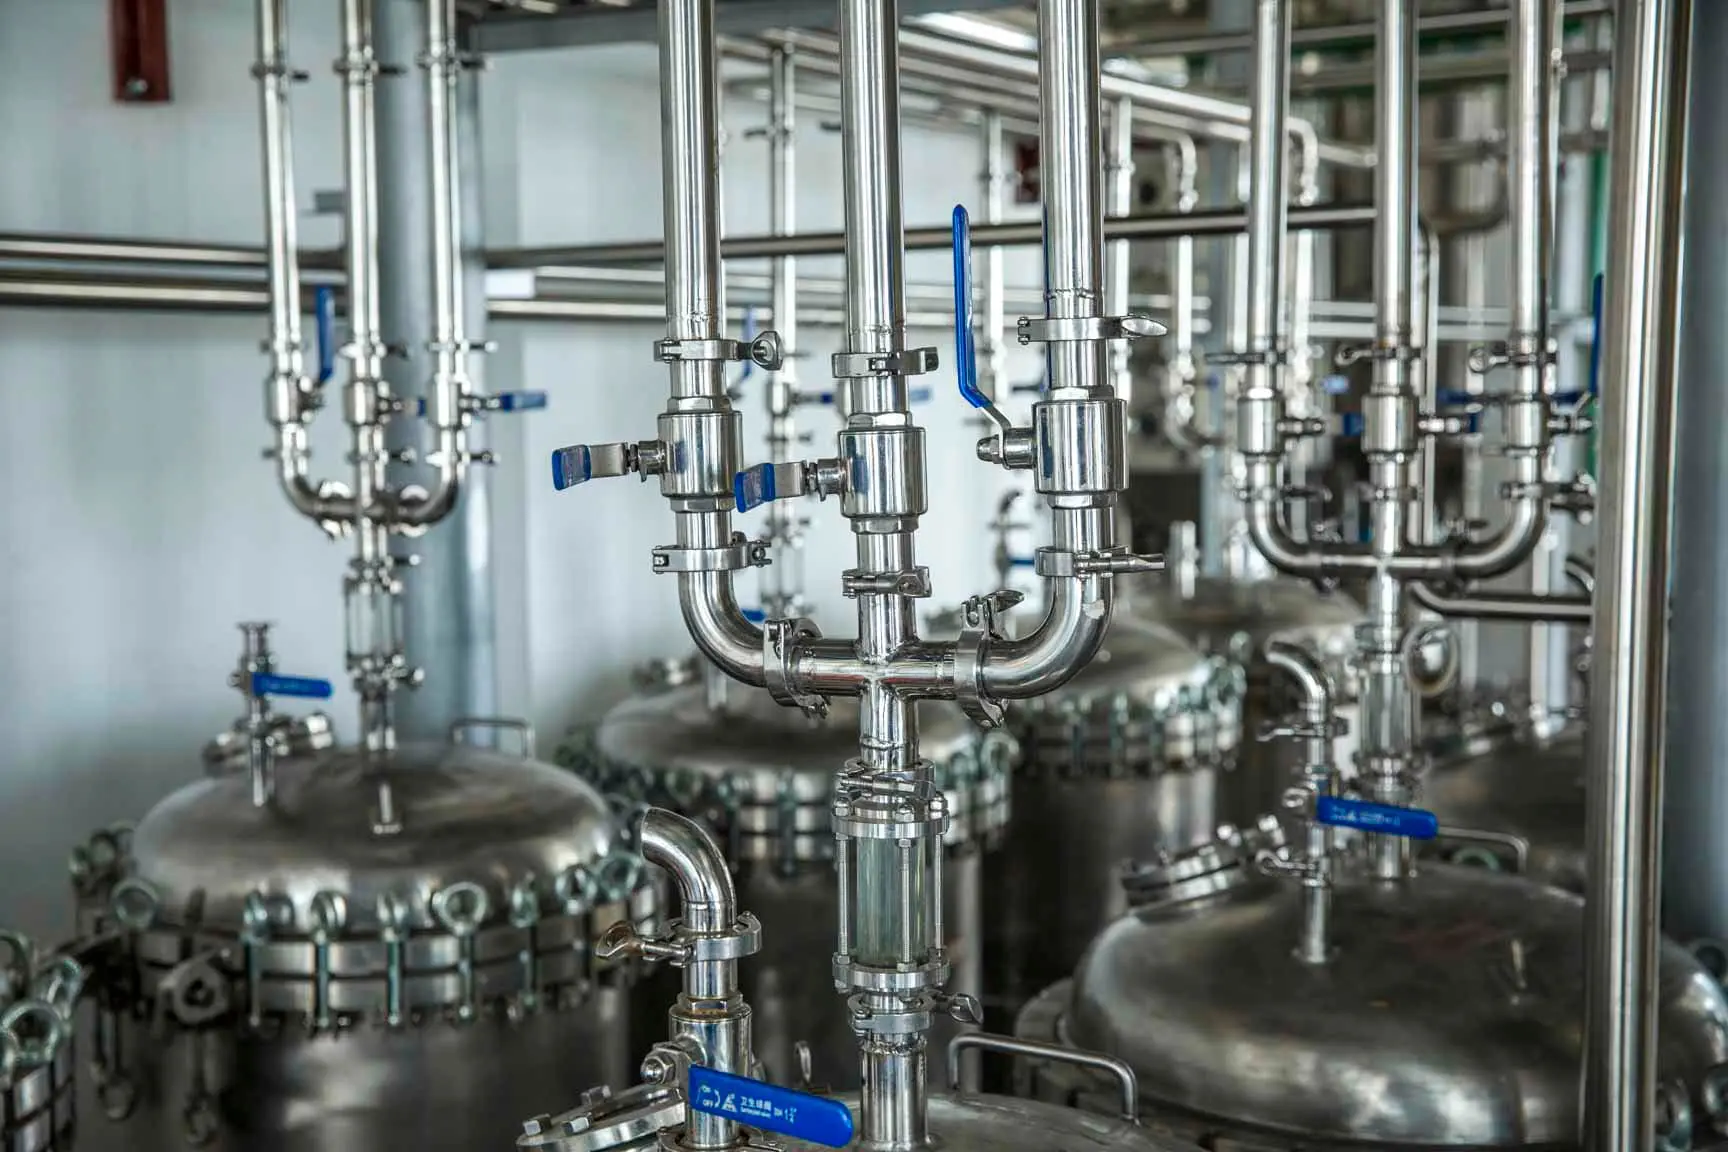
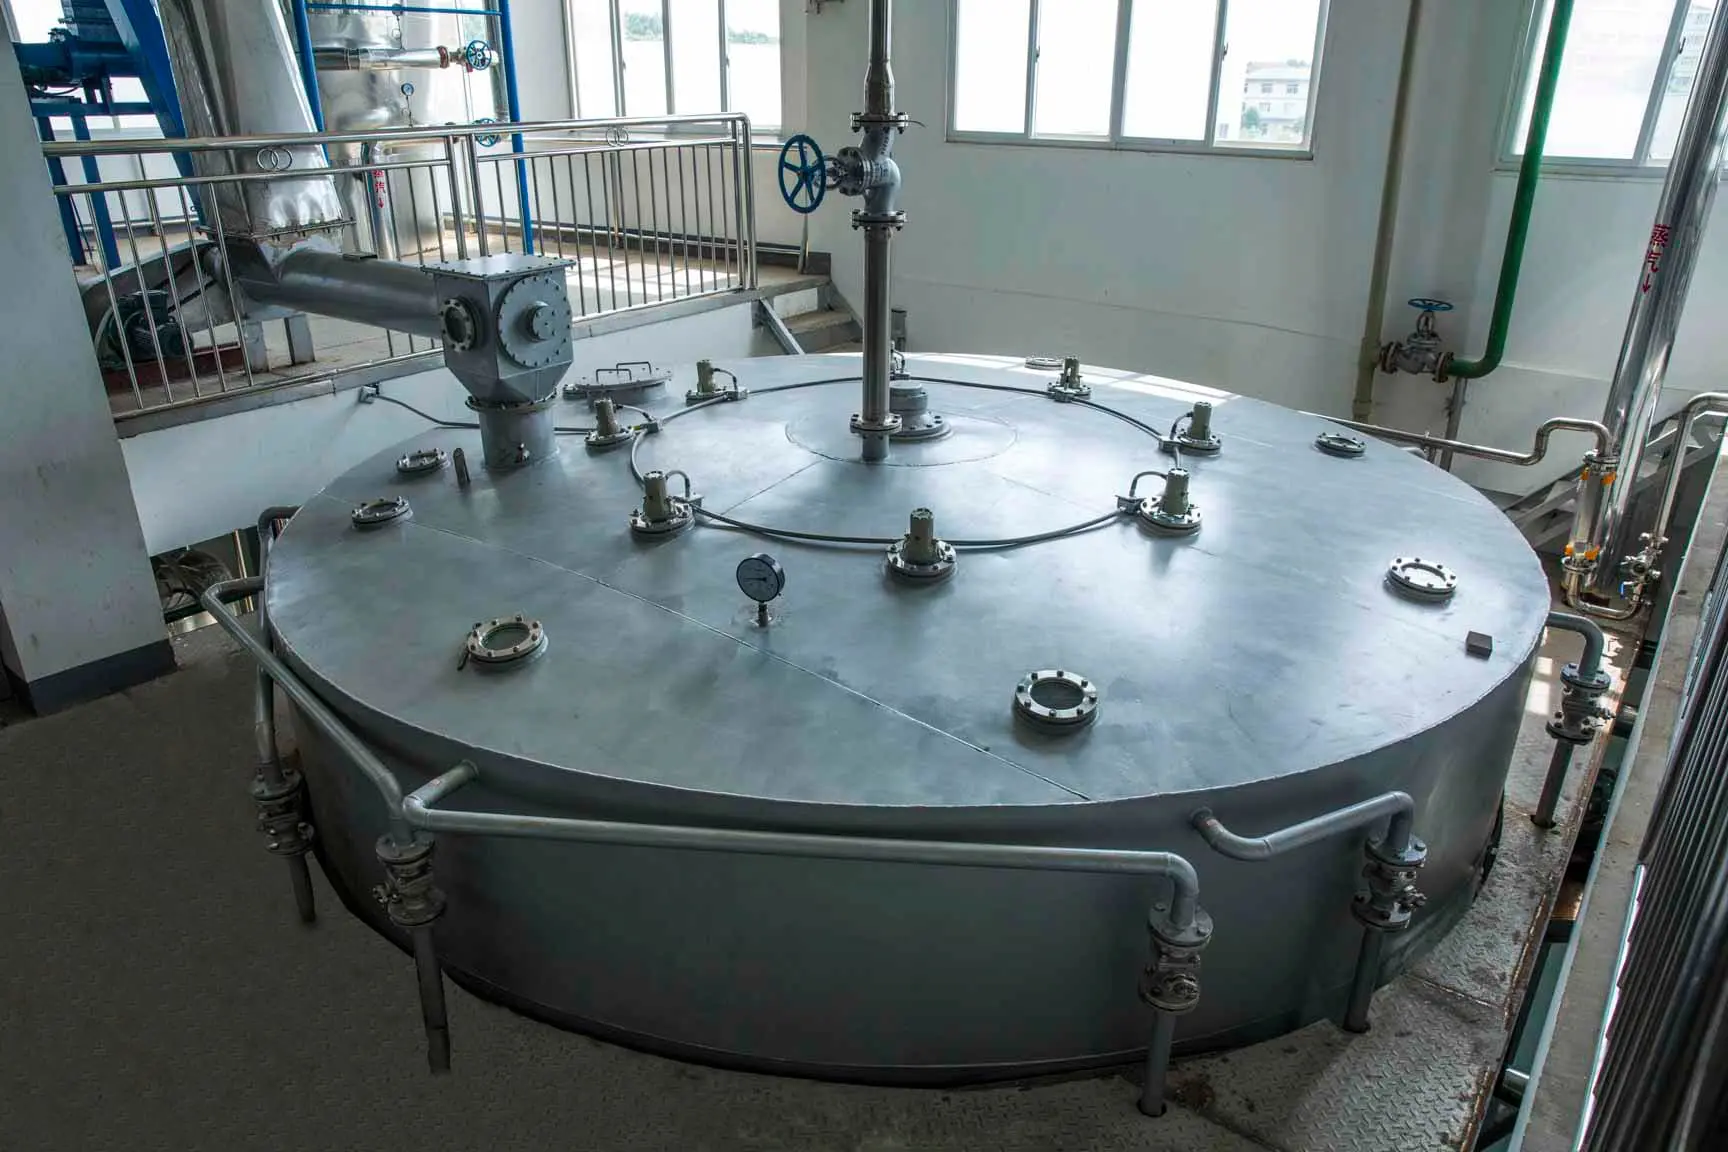
Our manufacturing network includes three advanced production facilities with a combined annual production capacity of 5,000+ tons. The facilities are operated under strict quality management systems to ensure stable production and consistent product quality.
Comprehensive process traceability and batch-specific testing are implemented throughout production, with key parameters such as active ingredient content, pesticide residues, solvent residues, and Benzo[a]pyrene controlled to meet Chinese, European, and U.S. requirements.


Advanced Testing Equipment
Our facilities are equipped with professional extraction, concentration, drying, blending, and testing equipment, supporting both standard botanical extracts and customized formulations.
Advanced production and laboratory capabilities enable us to maintain precise process control, batch consistency, and comprehensive quality testing throughout the manufacturing process.
We provide batch testing for active ingredients, microbiological parameters, heavy metals, pesticides, ethylene oxide, solvent residues, and other customer-specific requirements, supporting reliable export-grade compliance.


Online Message